Edge AI cameras · Updated October 2026
What machine vision cameras are used for
What a machine vision camera is, how it turns a frame into a decision, where it is used on and off the factory floor, and which kind of camera fits which job.
Quick answers
- What is a machine vision camera? A camera whose pictures are read by software that makes a decision, such as pass or fail, a count or an alert, instead of by a person. How it works
- What are machine vision cameras used for? Inspecting and guiding on factory lines, watching the road and the driver in cars, sorting waste by material, and counting crops, livestock and wild animals. The uses
- What is a smart camera in machine vision? A camera that runs the vision model itself and sends out only the result, so no PC has to sit beside it. Smart camera or PC
- Which machine vision camera should you pick? Battery or solar sites with one thing to spot suit a microcontroller camera; lines with several objects or extra sensors suit a Linux camera with a neural accelerator. Pick a camera
- Is there an affordable machine vision camera? Our open-source Tokay Lite costs $102 on CrowdSupply and is also sold on Mouser; Tokay Pro is supplied by quote. Prices
- $60 bnprojected computer vision market by 2030, per Grand View Research
- 24%of automotive manufacturers use machine vision now, per a Zebra survey
- 44%of automotive manufacturers plan to use it by 2027, same survey
- 2 bn tof waste thrown away each year, which cameras help sort for recycling
What is a machine vision camera?
It is the eye of a system that looks, decides and acts without a person in the loop. The camera supplies the frames; a vision model reads them and reports what it found.
Machine vision is the branch of artificial intelligence that lets machines observe a scene, analyze it and respond. A model trained on many labelled images learns what a good part, a road sign or a plastic bottle looks like, and the camera feeds it new frames to judge.
The camera can be as simple as the ones in a parking lot or on a car dashboard. Industrial machine vision cameras are built for the plant floor instead: sealed housings, wider temperature ratings, and a processor and network link on board so the result can go straight to a controller or a phone.
Smart camera or camera plus PC?
The oldest systems stream video to a PC that runs fixed rules. A smart camera runs the model inside and sends out only the answer. Both are still sold, and they suit different jobs.
Camera plus PC
An industrial camera sends every frame over Gigabit Ethernet or USB to a vision PC next to the line. The PC runs the inspection software and talks to the line controller.
It fits a plant that already has a vision PC and an engineer who maintains it. The cost is a PC per station, the cabling, and a stream of full frames over the network.
Smart camera
The processor and a neural accelerator sit inside the camera. It runs the model on each frame and sends a result, an event or a short clip over Wi-Fi, MQTT or a USB link.
It fits places where a PC would be in the way or cannot go: a roof, a field, a gate, or a line where each station should stand alone. Tokay Pro is our smart camera for lines; Tokay Lite is the battery version.
What are machine vision cameras used for?
Factories were first, but the same camera and model pattern now runs in cars, recycling plants, farms and nature reserves. Each card below is covered in more detail further down.
Manufacturing
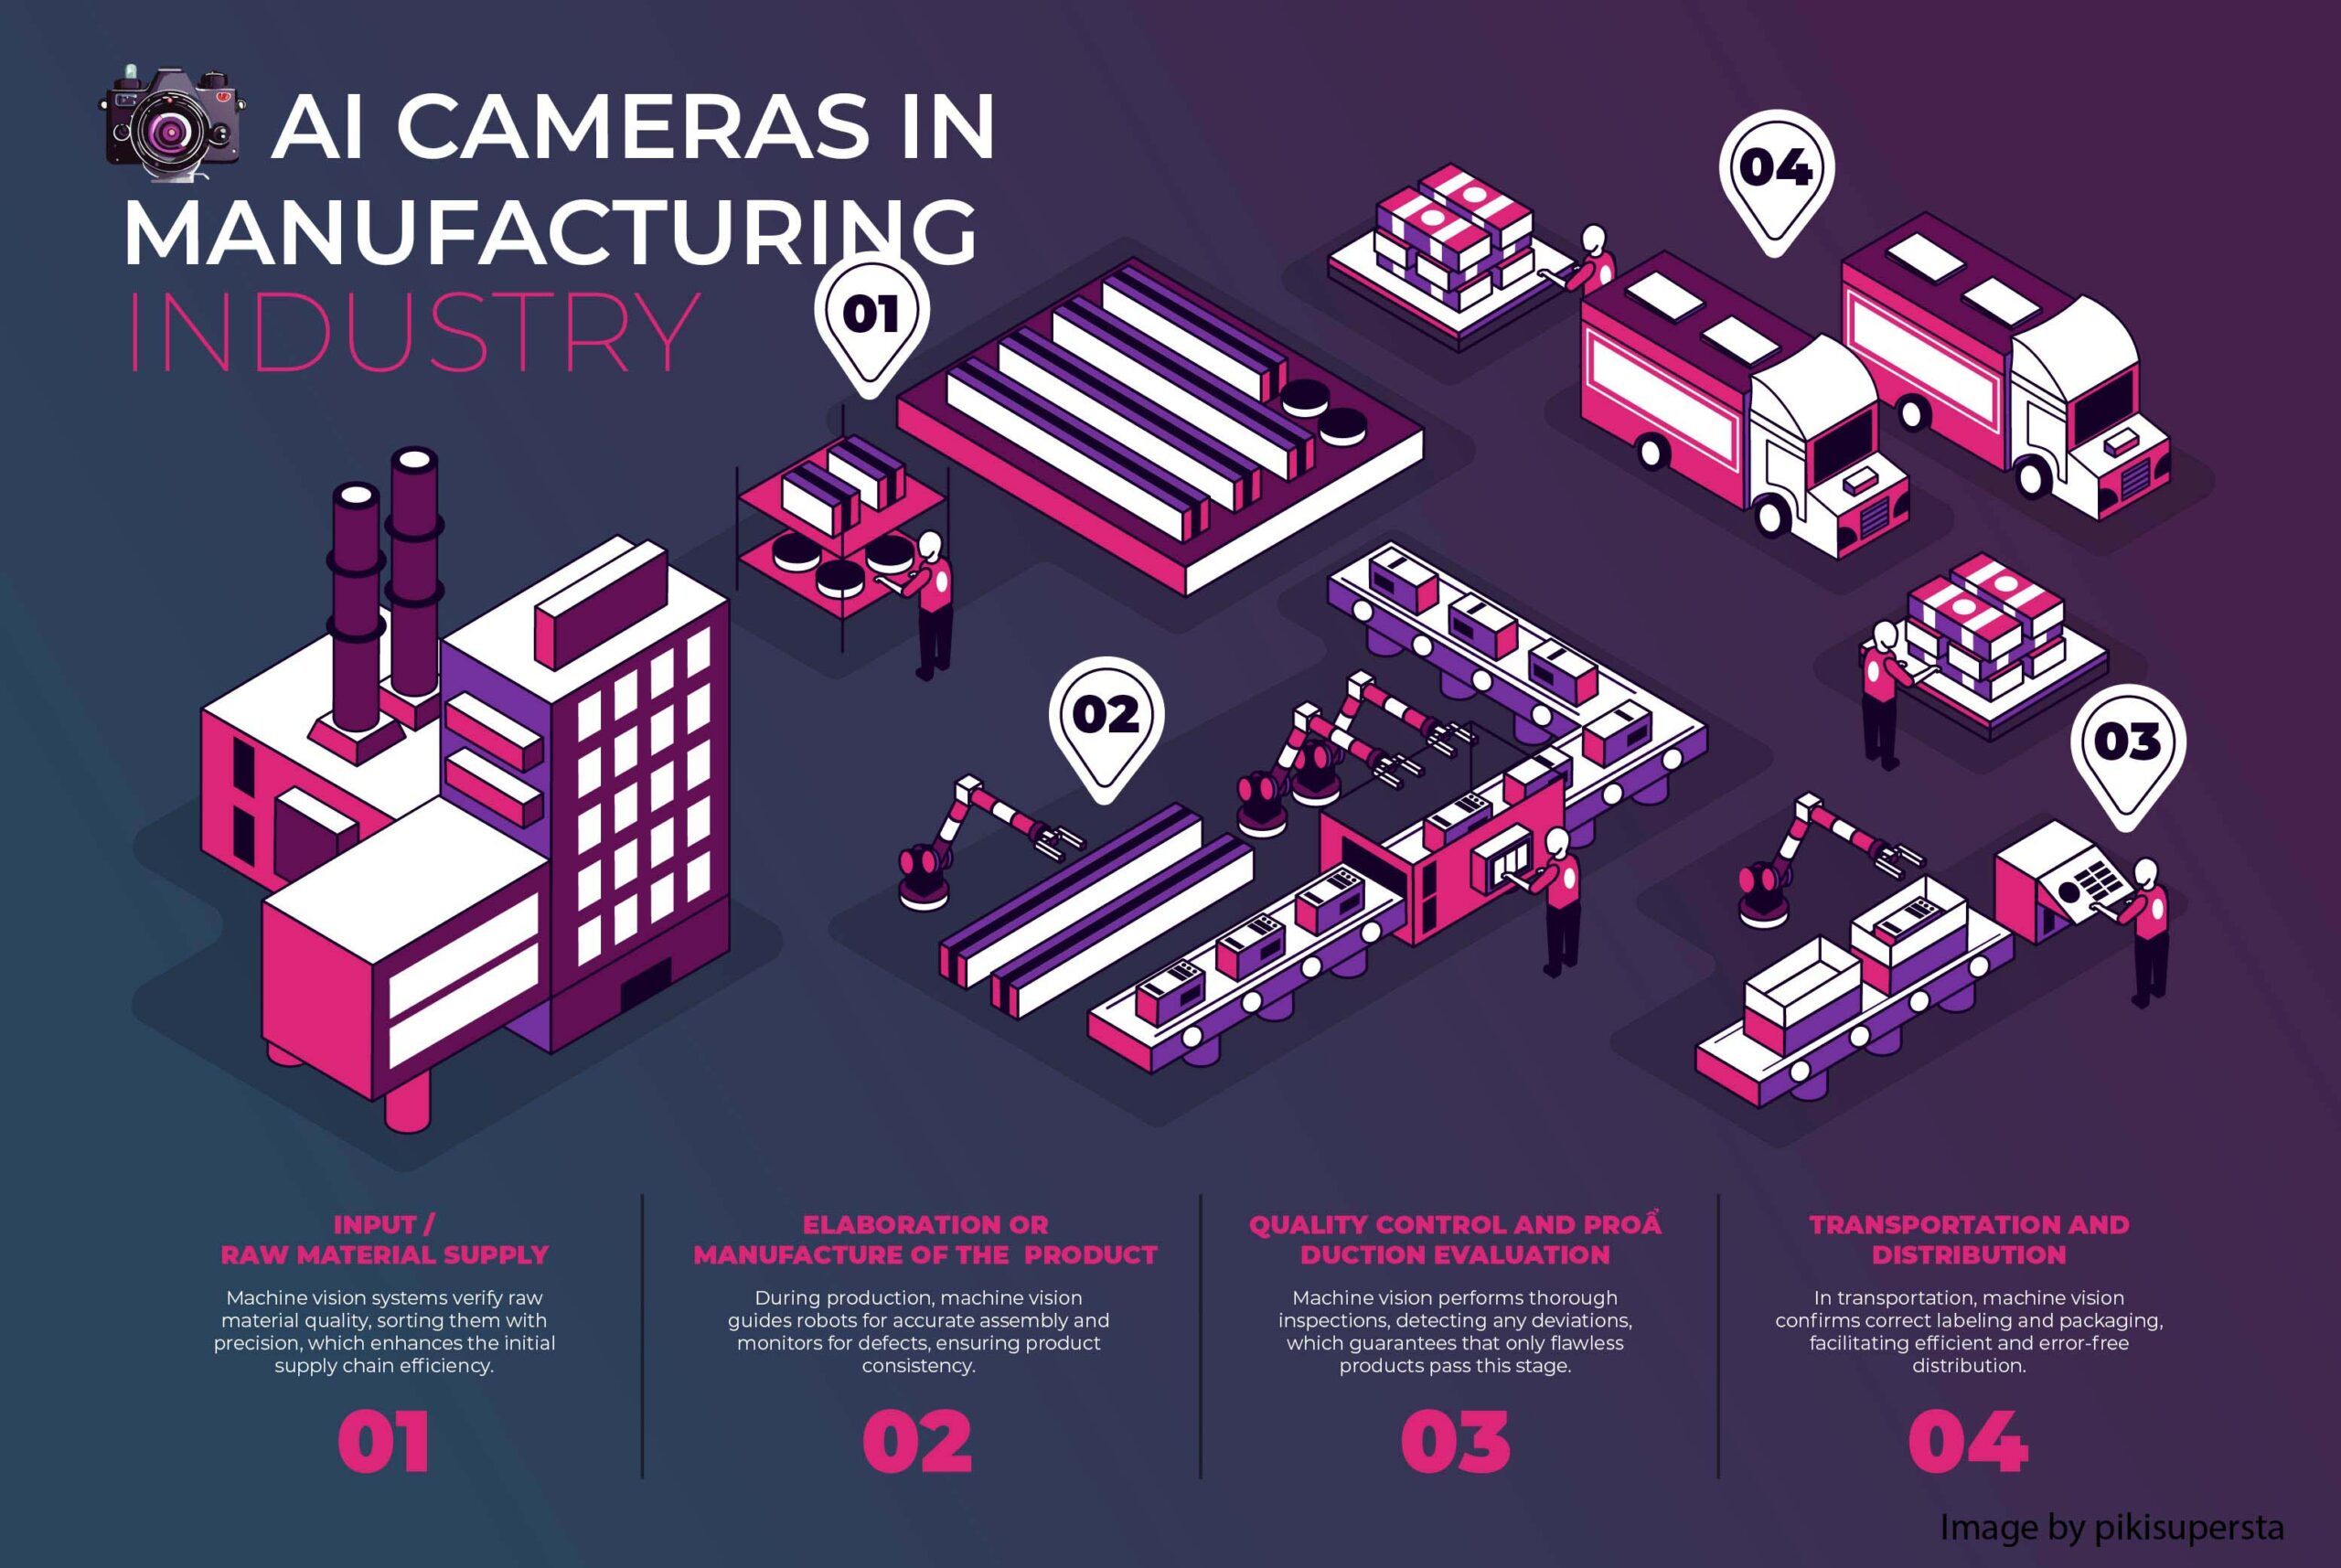
Detecting and counting parts, guiding robots, measuring, checking labels and spotting defects before a product ships.
Automotive
Finding scratches and checking coatings at the plant, then reading the road and watching the driver once the car is sold.
Recycling
Classifying each item on a waste belt by material and telling a picking robot which ones to pull.
Agriculture
Counting and watching livestock, finding weeds and diseased plants, and grading produce.
Wildlife monitoring
Camera traps that wake on motion, take a picture at night and identify the species without a person sorting the photos.
Parking and sites
Counting free spaces, reading plates and flagging people where they should not be. Our smart parking article covers it.
How do factories use machine vision cameras?
A factory floor has many things moving at once, and a camera checks every part to the same standard on every shift. Industrial cameras are mounted over conveyors and inside robot cells, where they feed a vision model that drives these tasks:
- detecting, recognizing, sorting and counting objects
- guiding machinery and robot arms
- inspecting parts for defects and taking measurements
- checking packaging and labels
- spotting a malfunction and watching that safety rules are followed
The payoff is fewer bad parts reaching a customer and fewer people doing repetitive checks. Our article on how AI cameras are used in manufacturing goes through each task on the line, the camera types factories use and what to check before buying.
How do cars and car plants use machine vision?
Vision runs from the production line to the road. A survey by Zebra Technologies found 24% of automotive manufacturers using machine vision and 44% planning to by 2027.
In the plant
Cars are built in large numbers to strict quality limits, so a fault that slips through is expensive. Cameras spot scratches on machined surfaces, identify and inspect parts and coatings, and keep a record for quality control.
On the road
Dashboard cameras combined with sensors such as lidar let vision models see the road ahead: hazards, road signs and speed limits, with a warning before a likely collision.
Inside the cabin
A cabin camera builds a 3D depth map of the driver's head, face and eyes and alerts them when they look away; distraction is one of the main causes of crashes. The same camera can check hands on the wheel, seatbelts and which seats are occupied, and adjust how an airbag opens to the way someone sits.
How do machine vision cameras sort waste for recycling?
A camera over the belt identifies each item and what it is made of, then a robot picks it out. The plant recycles more of what arrives and keeps a record of the type and amount of waste.
The world throws away over 2 billion tons of waste a year, a figure the World Bank expects to grow by 70% by 2050, and only around 30 percent of it is recycled.
Sorting plants use cameras to scan every item, decide whether it can be recycled and send the answer to a database or to a picking robot. The common technique is semantic segmentation: the model labels each pixel of the image by material.
Plastics are hard to tell apart in visible light. Spectral cameras see beyond the visible range and separate plastics by their chemical composition. The same principle lets a camera see methane, which we cover in hyperspectral cameras in gas detection.
How are machine vision cameras used on farms and in wildlife surveys?
Outdoors the camera usually runs on a battery or a solar panel, far from a network cable. It has to wake on its own, see at night and send a short result over a radio.
Wildlife monitoring
Wild animals are shy, often active at night and spread over large areas, and sorting the photos afterward is a bigger job than taking them. A camera trap wakes on a motion sensor, takes a picture with infrared light at night, and the model labels the species so researchers only review the frames that matter.
Tokay Lite suits this job: a PIR motion sensor wakes it, IR LEDs light the scene to about 10 m, and it sleeps on microamps between events.
Agriculture
Farms have to feed a population heading for 10 billion by 2050 with a shrinking workforce. Cameras count and classify livestock without handling them and watch feed, water and behavior, which can flag an outbreak early.
For crops, drones with cameras find weeds and spray herbicide only where it is needed, and spectral cameras tell plant species apart and grade produce. Cameras also detect disease in produce, track irrigation channels and help predict harvest time. More in IoT in agriculture and how a smart farm works.
Which machine vision camera fits the job?
Start from the power supply and the number of things the camera must recognize in one frame. Those two answers usually decide the platform before resolution or price comes up.
| The job | Camera that fits | Why | Price |
|---|---|---|---|
| Battery or solar site, one thing to spot: a gate, a roof, a camera trap | Tokay Lite, ESP32-S3 | Wakes on motion or a timer, runs face or object detection at 1 to 10 fps, sleeps on microamps; −40 to +50 °C | $102 on CrowdSupply, also on Mouser |
| Line or site with several objects per frame, or thermal and spectral beside visible | Tokay Pro, NXP i.MX 8M Plus | 2.3 TOPS accelerator, Linux, three MIPI-CSI sensor ports, 8 MP IMX219 as standard; module rated −40 to +85 °C | By quote |
| Fast line that already has a vision PC and software | Industrial GigE or USB camera feeding that PC | Keeps the existing software and the engineer who maintains it | Camera, lens, lighting and PC per station |
If you are comparing a hobby board for a first prototype, our ESP32-CAM vs Tokay Lite page shows what changes when the camera has to run for months on a battery.
Where this applies at Maxlab
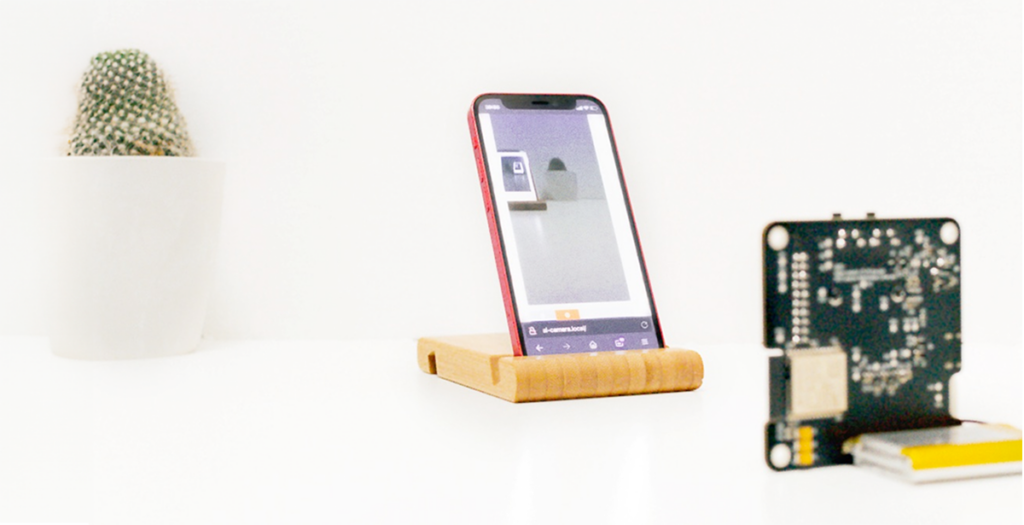
We make two machine vision cameras. Tokay Lite is an open-source ESP32-S3 camera for battery and solar sites, with a PIR sensor, IR night vision and 8 MB of PSRAM for the frame and the model; the schematic and SDK are on GitHub. Tokay Pro runs Linux on the i.MX 8M Plus and takes up to three sensors at once for lines and sites where a microcontroller is not enough.
The same platform went into a client's solar-powered roof camera: 9,500 units shipped, about six months per charge. If your project needs a camera of its own, with a different sensor, enclosure or firmware, that is what our hardware and firmware services cover.
- Tokay Lite
- ESP32-S3, PIR wake, IR to 10 m, Mouser and CrowdSupply
- Tokay Pro
- i.MX 8M Plus, 2.3 TOPS, three sensor ports, by quote
- Roof camera
- 9,500 units shipped, about six months per charge
- Open source
- CERN-OHL-P-2.0 hardware, Apache 2.0 SDK
Tell us what your camera has to see
Send what the camera must recognize, where it will be mounted and how it is powered, and we will say which platform fits and what a first unit involves. We reply within 24 hours.
Or email [email protected] or book a 30-minute call.
Common questions
What is a machine vision camera?
A machine vision camera captures images for software to judge rather than for a person to watch. A vision model reads each frame and returns a decision, such as pass or fail, a count, a measurement or an alert, which then drives a robot, a reject arm or a notification. Industrial versions add a sealed housing, a wider temperature rating and a network link.
What is the difference between machine vision and computer vision?
Computer vision is the general field of teaching computers to interpret images. Machine vision is computer vision put to work in a machine: a camera, a model and an output wired to something that acts, usually on a production line, a vehicle or a site.
What does a smart camera do?
A smart camera runs the vision model on its own processor and sends out the result instead of the video. That removes the PC from the station and cuts the network traffic to a few bytes per event. Tokay Pro does this on a 2.3 TOPS neural accelerator; Tokay Lite does it on an ESP32-S3 for battery sites.
What are the best industrial cameras for machine vision?
The best camera is the one that matches the power supply, the number of objects per frame and the sensors you need. A battery or solar site with one thing to detect suits a microcontroller camera that sleeps between events. A line that tracks several objects, or needs thermal or spectral images beside visible ones, needs a Linux camera with a neural accelerator. A plant with an existing vision PC can keep it and add a GigE or USB camera.
How much do machine vision systems cost?
A PC-based system costs a camera, a lens, lighting, a PC and the inspection software for every station. A smart camera folds the PC into the camera. Our Tokay Lite costs $102 on CrowdSupply and is sold on Mouser as TOKAY-LITE-01. Tokay Pro is priced by quote, depending on quantity, sensors and whether we build the enclosure and firmware.
Is there an affordable or cheap machine vision camera?
Yes, for jobs where one kind of object has to be spotted. Tokay Lite is an open-source ESP32-S3 camera that runs face or object detection on the board at 1 to 10 frames per second, and its schematic and SDK are on GitHub. The ESP32-CAM vs Tokay Lite page compares it with the cheapest hobby boards.
How big is the machine vision camera market?
Grand View Research projects the wider computer vision market at almost $60 billion by 2030. Adoption is still growing: in a Zebra Technologies survey, 24% of automotive manufacturers used machine vision and 44% planned to by 2027.
Where does machine vision fit in Industry 4.0?
Industry 4.0 means connected machines that share data and act on it. Machine vision cameras supply much of that data from the line: what passed, what failed, how many, and when a machine started behaving differently.
Can machine vision cameras see in the dark?
Yes, with infrared light or a thermal sensor. Tokay Lite has IR LEDs that light a scene to about 10 m and switches its IR-cut filter at night. Tokay Pro can take a thermal sensor next to its visible camera, which records heat rather than reflected light.
How are machine vision cameras used in cars?
In the plant they find scratches and check parts and coatings. On the road, dashboard cameras with lidar read hazards, signs and speed limits. In the cabin, a camera tracks the driver's head and eyes to warn of distraction and checks seatbelts, hands on the wheel and seat occupancy.